Industrial operations that consume acetone every day face a constant balancing act. Production teams need enough clean solvent to keep equipment and processes moving, while facility managers must control purchasing costs and spent solvent volumes. As acetone use rises, that balance can become harder to maintain with small containers or irregular recovery practices.
A 55-gallon recovery unit provides high-volume operations with a practical way to manage larger quantities of spent acetone on-site. Rather than treating used acetone as a one-way expense, facilities can integrate recovery into their normal production routine. That approach can help teams reduce solvent purchases while gaining greater control over waste handling. Here’s how to manage daily acetone use with 55-gallon units.
Match Capacity To Daily Use
Daily acetone consumption should guide equipment selection. A facility that generates substantial quantities of contaminated acetone needs sufficient recovery capacity to keep pace with production. If recovery equipment handles too little solvent at a time, spent material can accumulate faster than operators can process it.
A 55-gallon unit addresses that problem by providing industrial users with sufficient batch capacity for heavier solvent loads. Solvent Waste Management’s Model SW 55 can process up to 55 gallons per batch. That capacity makes the unit suitable for operations that regularly generate large volumes of contaminated acetone.
Facilities still need to consider how quickly they create spent solvent. Managers can compare normal acetone consumption with expected recovery cycles and available storage. That comparison helps the operation establish a routine that supports production without allowing excessive waste to pile up.
Build Recovery Into the Workflow
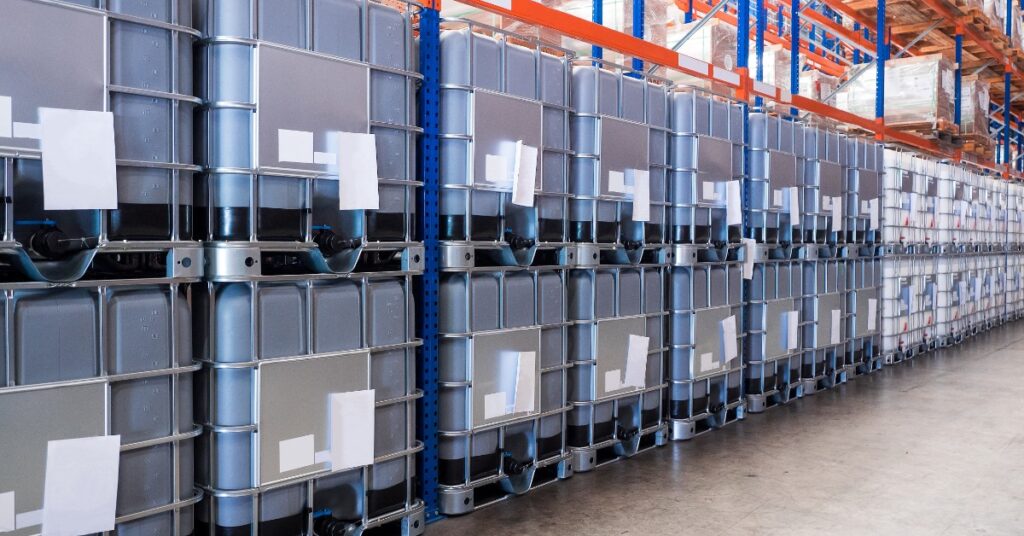
Solvent recovery works best when operators treat it as part of the normal production process rather than an occasional waste project. Teams can collect spent acetone from approved processes and transfer it to the recovery unit in accordance with facility procedures. A consistent schedule helps operators manage solvent volumes before storage containers take over valuable floor space.
An acetone recycling machine uses distillation to separate usable acetone from contaminants. The system heats contaminated solvent so the acetone vaporizes, then condenses the vapor back into liquid. Residue remains behind while operators collect the recovered solvent for appropriate reuse.
The SW 55 uses vacuum assistance to lower the solvent’s boiling point during processing. Its automatic feed also pumps contaminated solvent into the unit. These features support facilities that want to handle larger batches without adding unnecessary manual steps to each recovery cycle.
Reduce Fresh Acetone Purchases
High-volume acetone users can spend a significant share of their operating budget replacing solvent that leaves the facility as waste. Recovery offers those businesses another option. When a facility can reuse suitable recovered acetone, it reduces the amount of virgin solvent it needs to purchase for compatible applications.
The financial impact varies by each operation’s acetone consumption, solvent condition, and disposal practices. Facilities with frequent solvent turnover often have more opportunities to recover usable material. Managers should review their purchasing and waste records rather than relying on broad savings estimates.
Regular recovery can also make solvent purchasing more predictable. When teams know how much acetone they typically reclaim, purchasing departments can plan orders around real consumption instead of replacing every gallon that enters the waste stream. That visibility supports tighter inventory control.
Control Spent Solvent Volumes
Purchasing represents only one side of daily acetone management. Facilities must also deal with the contaminated material that remains after cleaning or production tasks. When a company sends all spent solvent out for disposal, higher acetone use usually creates greater waste volume.
On-site recovery reduces the amount of solvent entering the disposal stream by separating reusable acetone from contaminants. Operators still need to handle the remaining residue in accordance with applicable facility procedures and regulations. However, recovery can change the volume and composition of material requiring disposal.
That reduction can benefit plants where spent solvent storage creates logistical pressure. Fewer full drums waiting for pickup can free space and simplify internal handling. Environmental and safety managers can also gain a clearer view of how solvent moves through the operation.
Keep Operation Straightforward
A recovery system needs to fit the pace of a busy industrial facility. Complicated equipment can discourage consistent use when operators already manage production demands. Straightforward controls help teams incorporate solvent recovery without turning the process into a separate labor-intensive task.
The SW 55 uses an automatic timer shutdown at the end of a cycle. It also places the distillation tank at a convenient working height and uses a tilt-back lid with a quick-open feature. Disposable high-temperature bags and a tapered stainless steel tank support cleanup after processing.
The unit can gravity-feed recovered solvent into a 55-gallon drum. This arrangement suits facilities that already use standard drums for solvent storage or distribution. Operators can return recovered acetone to the facility’s solvent management process without relying on a complex transfer setup.
Plan for Consistent Processing
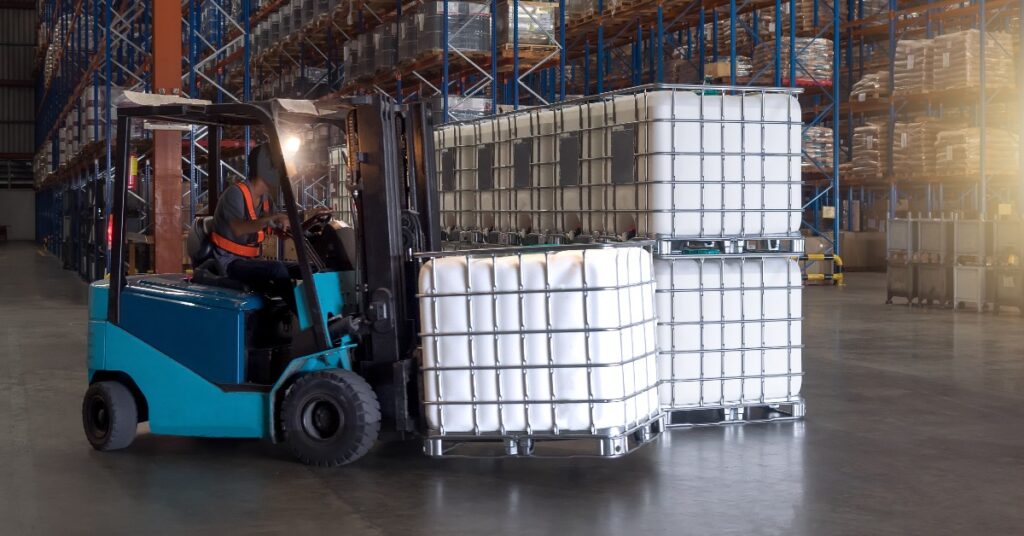
Capacity alone won’t improve acetone management if a facility doesn’t establish a practical operating schedule. Teams should identify when they generate the most spent solvent and schedule recovery cycles around those production patterns. A finishing operation may generate predictable volumes after cleaning spray equipment, while another facility may see solvent use fluctuate with production runs.
Operators should avoid waiting until storage becomes crowded before running the recovery unit. A regular rhythm keeps contaminated acetone moving through the process and gives managers a more accurate picture of recovery performance. Facilities can then adjust their schedule when production volume changes.
Consistent processing also helps teams identify unusual shifts in solvent consumption. If spent acetone volume suddenly increases, managers can review production practices and cleaning procedures to identify the source of the increase. Recovery equipment becomes part of a broader solvent management strategy rather than simply a waste-handling tool.
Support High-Volume Operations
Many industries rely on acetone for cleaning and production support. Paint operations, composite manufacturers, cabinet shops, and boat manufacturers may use substantial solvent volumes depending on their processes. For facilities with steady demand, small-scale recovery equipment may not align with the amount of solvent moving through the plant.
A 55-gallon system gives larger users room to process more material in each batch. That capacity can reduce the frequency of small recovery runs while helping teams keep up with routine solvent generation. The right schedule will still depend on the facility’s workload and acetone use.
Managers should look at the complete solvent cycle when considering equipment capacity. Purchasing records can show how much new acetone enters the facility, while waste records can reveal how much leaves. Comparing those numbers helps a business determine whether a 55-gallon recovery system fits its daily operation.
Create a Better Acetone Routine
55-gallon units can manage daily acetone use in all the right ways. High-volume facilities can recover usable solvent on-site and return it to suitable processes while reducing the amount of new acetone they purchase. A 55-gallon unit gives heavy users enough capacity to make that approach part of routine production.
The strongest results come from matching recovery capacity with real solvent use and maintaining a consistent processing schedule. Facilities that understand their acetone flow can manage purchasing and waste more deliberately. Solvent Waste Management offers the SW 55 for operations that need an on-site recovery option designed around larger solvent volumes.